Lincoln Aviator: Rear End Sheet Metal Repairs / Removal and Installation - Back Panel and Reinforcement
Special Tool(s) /
General Equipment
| Resistance Spotwelding Equipment |
| Scraper for Straight Edges |
| Grinder |
| Hot Air Gun |
| 8 mm Drill Bit |
| MIG/MAG Welding Equipment |
| Spot Weld Drill Bit |
| Locking Pliers |
Materials
| Name |
Specification |
Metal Bonding Adhesive
TA-1, TA-1-B, 3M™ 08115, LORD Fusor® 108B |
-
|
Seam Sealer
TA-2-B, 3M™ 08308, LORD Fusor® 803DTM |
-
|
Flexible Foam Repair
3M™ 08463, LORD Fusor® 121 |
-
|
Removal
 WARNING:
Electric vehicles damaged by a crash may have compromised
high voltage safety systems and present a potential high voltage
electrical shock hazard. Exercise caution and wear appropriate Personal
Protective Equipment (PPE) safety gear, including high voltage safety
gloves and boots. Remove all metallic jewelry, including watches and
rings. Isolate the HV system as directed by the Ford Emergency Response
Guide for the vehicle. Failure to follow these instructions may result
in serious personal injury or death.
NOTICE:
The high-voltage battery in a Battery Electric Vehicle
(BEV), Hybrid Electric Vehicle (HEV) or Plug-In Hybrid Electric Vehicle
(PHEV) can be affected and damaged by excessively high temperatures. The
temperature in some body shop paint booths can exceed 60° C (140° F).
Therefore, during refinishing operations, the paint booth temperature
must set at or below 60° C (140° F) with a bake time of 45 minutes or
less. Temperatures in excess of 60° C (140° F) or bake durations longer
than 45 minutes will require the high-voltage battery be removed from
the vehicle prior to placing in the paint booth.
NOTICE:
Electric Vehicle (EV), Hybrid Electric Vehicle (HEV) and
Plug-In Hybrid Electric Vehicle (PHEV) vehicles contain a High Voltage
Battery (HVB). Before welding near the HVB, the HVB must be removed to
avoid heat damage.
-
Depower the SRS .
Refer to: Supplemental Restraint System (SRS) Depowering (501-20B Supplemental Restraint System, General Procedures).
-
Restore the vehicle to pre-accident dimensions, if required.
Refer to: Body and Frame (501-26 Body Repairs - Vehicle Specific Information and Tolerance Checks, Description and Operation).
-
Remove the rear bumper.
Refer to: Rear Bumper (501-19 Bumpers, Removal and Installation).
-
Remove the rear lamp assembly.
Refer to: Rear Lamp Assembly (417-01 Exterior Lighting, Removal and Installation).
-
Remove the loadspace trim panel.
Refer to: Loadspace Trim Panel (501-05 Interior Trim and Ornamentation, Removal and Installation).
-
Remove the auxiliary battery.
Refer to: Auxiliary Battery (414-01 Battery, Mounting and Cables, Removal and Installation).
-
Remove the side obstacle detection control module.
Refer to: Side Obstacle Detection Control Module (419-04 Side and Rear Vision, Removal and Installation).
-
Remove the rear lamp fade control module.
Refer to: Rear Lamp Fade Control Module (417-01 Exterior Lighting, Removal and Installation).
-
Remove the vehicle dynamics module.
Refer to: Vehicle Dynamics Control Module (VDM) (204-05 Vehicle Dynamic Suspension, Removal and Installation).
-
As Equipped:
Remove module and electronic devices as required for access to back panel and reinforcement.
-
Remove the liftgate striker.
-
Position the carpeting and the wiring harness away from the working area.
-
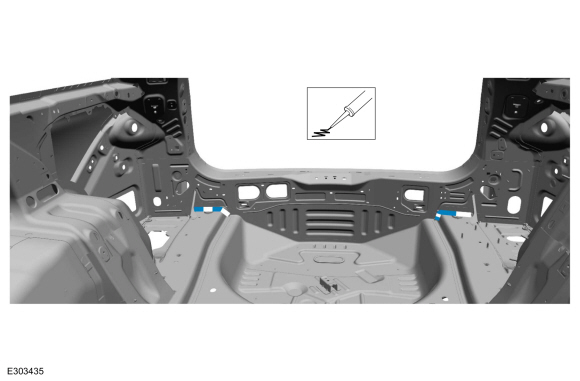
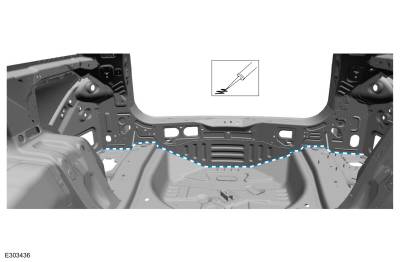
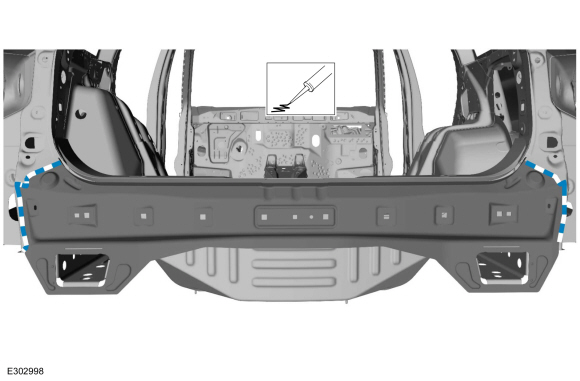
Remove the sealer using a grinder with an abrasive disc or equivalent.
Use the General Equipment: Grinder
-
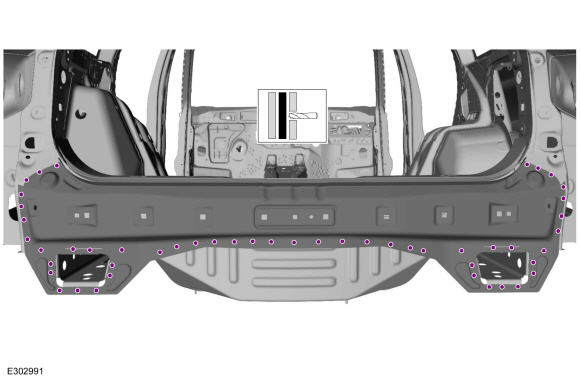
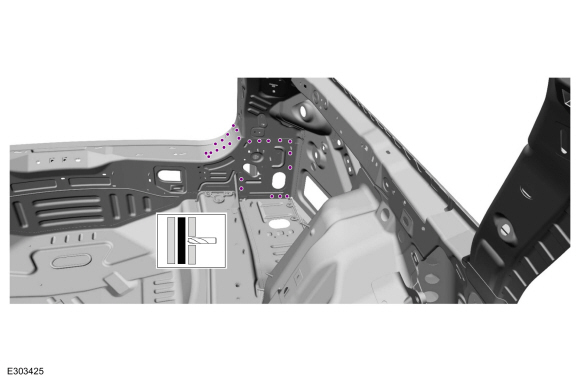
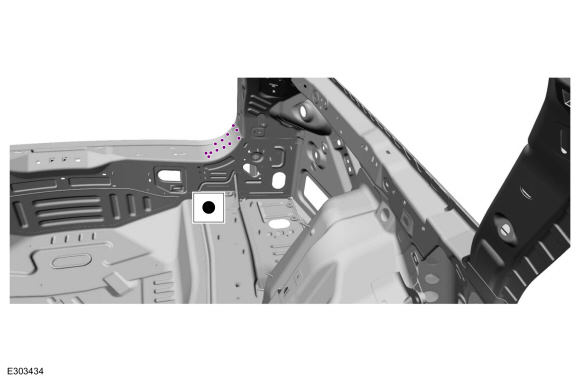
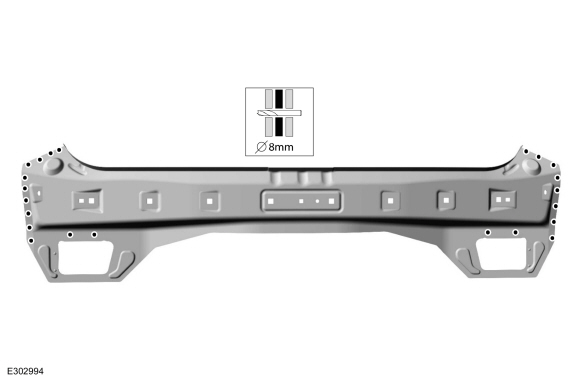
Remove the welds.
Use the General Equipment: Spot Weld Drill Bit
-
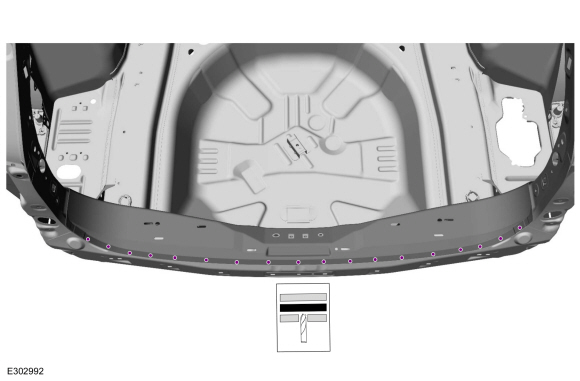
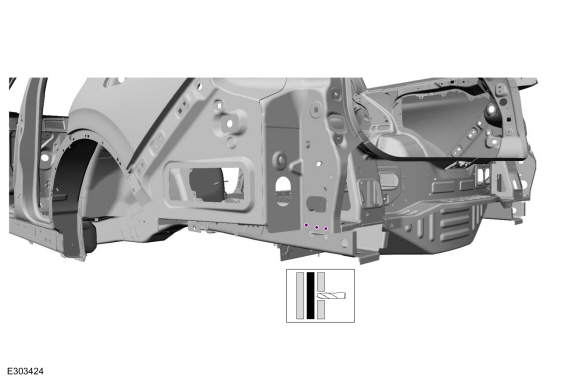
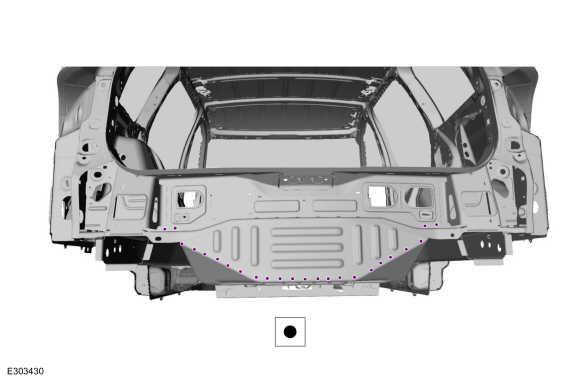
Remove the welds.
Use the General Equipment: Spot Weld Drill Bit
-
NOTE:
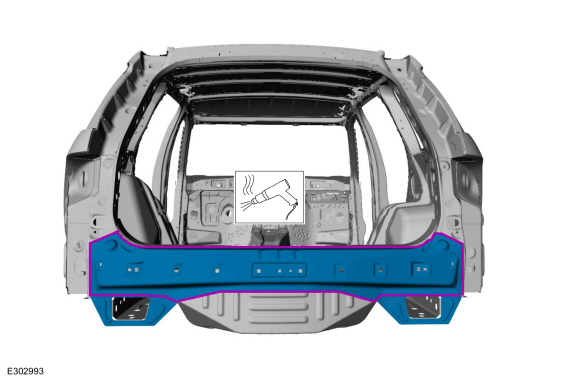
Use of a heat gun may aid in softening the adhesive.
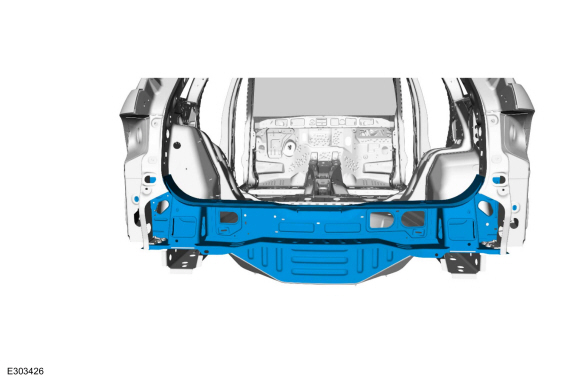
Remove the back panel.
Use the General Equipment: Hot Air Gun
-
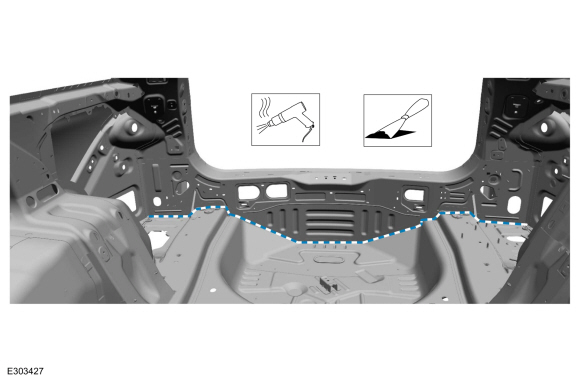
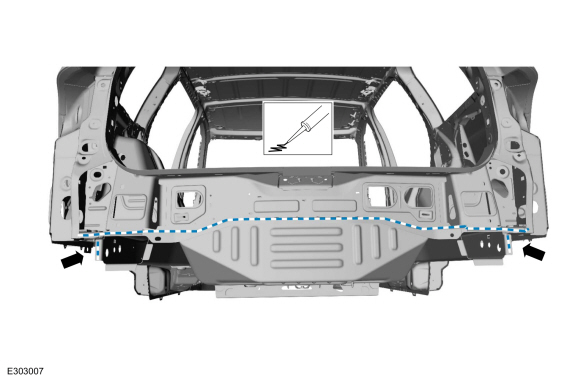
Remove the sealer and expandable foam.
Use the General Equipment: Hot Air Gun
Use the General Equipment: Scraper for Straight Edges
-
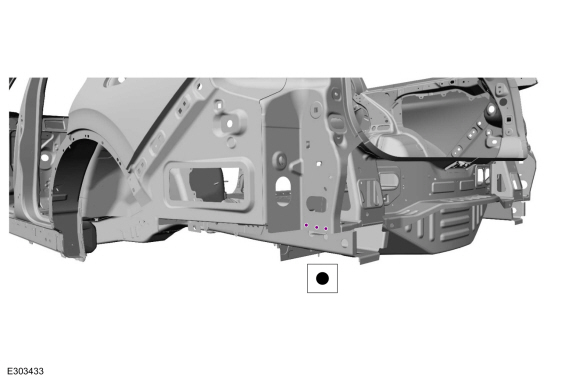
On Both Sides:
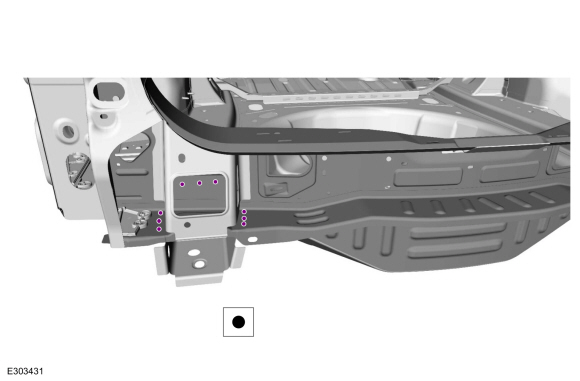
Remove the welds.
Use the General Equipment: Spot Weld Drill Bit
-
On Both Sides:
Remove the welds.
Use the General Equipment: Spot Weld Drill Bit
-
On Both Sides:
Remove the welds.
Use the General Equipment: Spot Weld Drill Bit
-
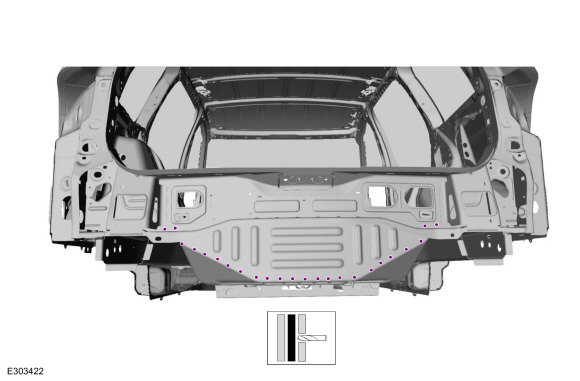
Remove the welds.
Use the General Equipment: Spot Weld Drill Bit
-
NOTE:
Pay particular attention to location of sealers and foams used to aid in installation.
Remove the back panel reinforcement.
Installation
WARNING:
Electric vehicles damaged by a crash may have compromised
high voltage safety systems and present a potential high voltage
electrical shock hazard. Exercise caution and wear appropriate Personal
Protective Equipment (PPE) safety gear, including high voltage safety
gloves and boots. Remove all metallic jewelry, including watches and
rings. Isolate the HV system as directed by the Ford Emergency Response
Guide for the vehicle. Failure to follow these instructions may result
in serious personal injury or death.
NOTICE:
The high-voltage battery in a BEV (Battery Electric
Vehicle), HEV (Hybrid Electric Vehicle) or PHEV (Plug-In Hybrid Electric
Vehicle) can be affected and damaged by excessively high temperatures.
The temperature in some body shop paint booths can exceed 60° C (140°
F). Therefore, during refinishing operations, the paint booth
temperature must set at or below 60° C (140° F) with a bake time of 45
minutes or less. Temperatures in excess of 60° C (140° F) or bake
durations longer than 45 minutes will require the high-voltage battery
be removed from the vehicle prior to placing in the paint booth.
NOTICE:
EV (Electric Vehicle), HEV (Hybrid Electric Vehicle) and
PHEV (Plug-In Hybrid Electric Vehicle) vehicles contain a HVB (High
Voltage Battery). Before welding near the HVB, the HVB must be removed
to avoid heat damage.
NOTICE:
If refinishing cure temperatures exceed 60°C (140°F), the charge port light ring must be removed.
NOTE:
Factory welds may be replaced with resistance spot welds or
MIG (metal inert gas) plug welds. Resistance spot welds may not be
placed directly over original location. They must be placed adjacent to
original location and equal factory welds in quantity. MIG (metal inert
gas) plug welds must equal factory welds in both location and quantity
-
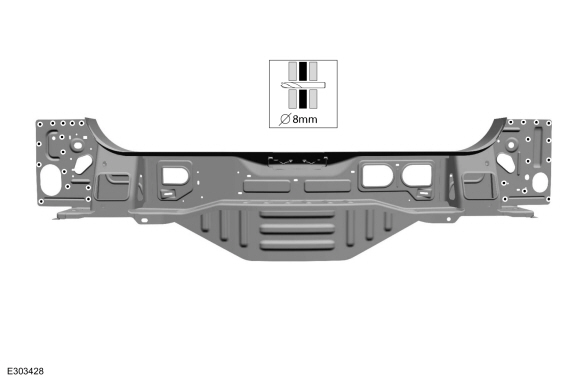
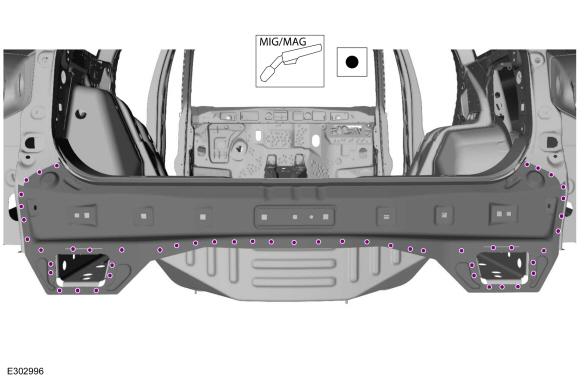
Drill holes for plug welding.
Use the General Equipment: 8 mm Drill Bit
-
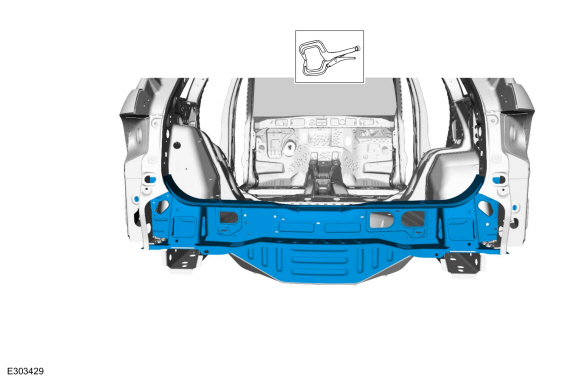
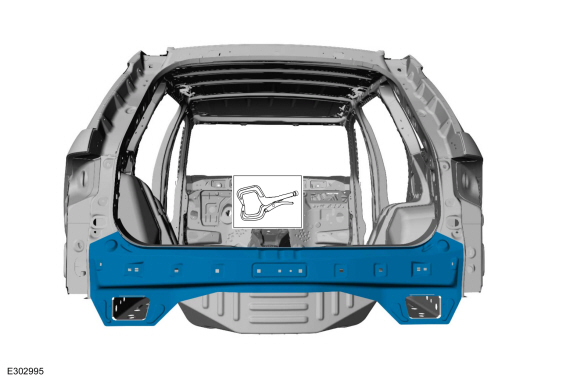
Install properly position and clamp the back panel reinforcement.
Use the General Equipment: Locking Pliers
-
On Both Sides:
Install the welds.
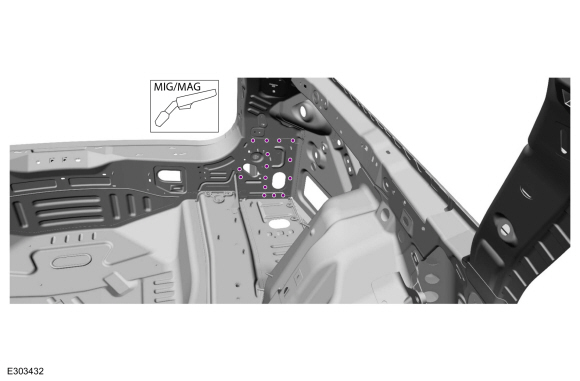
Use the General Equipment: MIG/MAG Welding Equipment
-
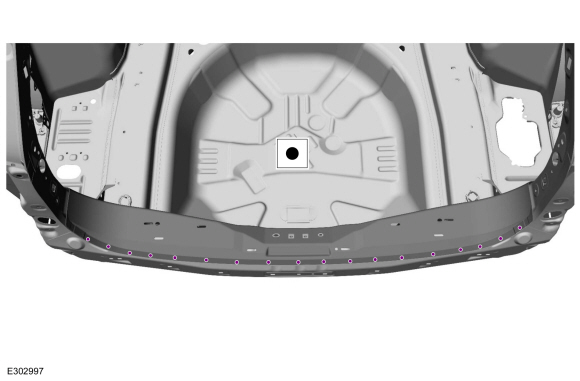
On Both Sides:
Install the welds.
Use the General Equipment: Resistance Spotwelding Equipment
-
On Both Sides:
Install the welds.
Use the General Equipment: Resistance Spotwelding Equipment
-
On Both Sides:
Install the welds.
Use the General Equipment: Resistance Spotwelding Equipment
-
Install the welds.
Use the General Equipment: Resistance Spotwelding Equipment
-
Metal finish the repair area using typical metal finishing procedures.
-
Apply NVH in areas noted during removal.
Material: Flexible Foam Repair
/ 3M™ 08463, LORD Fusor® 121
-
Seam Sealing:
All seams must be sealed to production level.
Material: Seam Sealer
/ TA-2-B, 3M™ 08308, LORD Fusor® 803DTM
-
Drill holes for plug welding.
Use the General Equipment: 8 mm Drill Bit
-
Apply adhesive to mating surfaces.
Material: Metal Bonding Adhesive
/ TA-1, TA-1-B, 3M™ 08115, LORD Fusor® 108B
-
Install, properly position and clamp the panel in place.
Use the General Equipment: Locking Pliers
-
Weld the panel.
Use the General Equipment: Resistance Spotwelding Equipment
Use the General Equipment: MIG/MAG Welding Equipment
-
Weld the upper flange.
Use the General Equipment: Resistance Spotwelding Equipment
-
Metal finish the repair area using typical metal finishing procedures.
-
Seam Sealing:
All areas must be sealed to production level.
Material: Seam Sealer
/ TA-2-B, 3M™ 08308, LORD Fusor® 803DTM
-
Restore corrosion protection.
Refer to: Corrosion Prevention (501-25 Body Repairs - General Information, General Procedures).
-
Refinish using a Ford approved paint system.
-
Install the side obstacle detection control module.
Refer to: Side Obstacle Detection Control Module (419-04 Side and Rear Vision, Removal and Installation).
-
Install the rear lamp fade control module.
Refer to: Rear Lamp Fade Control Module (417-01 Exterior Lighting, Removal and Installation).
-
Install the vehicle dynamics module.
Refer to: Vehicle Dynamics Control Module (VDM) (204-05 Vehicle Dynamic Suspension, Removal and Installation).
-
As Equipped:
Install module and electronic devices as required.
-
Install the auxiliary battery.
Refer to: Auxiliary Battery (414-01 Battery, Mounting and Cables, Removal and Installation).
-
Reposition all wiring harnesses and carpeting.
-
Install the liftgate striker.
Torque:
18 lb.ft (25 Nm)
-
Install the rear bumper.
Refer to: Rear Bumper (501-19 Bumpers, Removal and Installation).
-
On Both Sides:
Install the rear lamp assembly.
Refer to: Rear Lamp Assembly (417-01 Exterior Lighting, Removal and Installation).
-
Install the loadspace trim panel.
Refer to: Loadspace Trim Panel (501-05 Interior Trim and Ornamentation, Removal and Installation).
Special Tool(s) /
General Equipment
Resistance Spotwelding Equipment
Scraper for Straight Edges
Hot Air Gun
8 mm Drill Bit
MIG/MAG Welding Equipment
Spot Weld Drill Bit
Materials
Name
Specification
Flexible Foam Repair3M™ 08463, LORD Fusor® 121
-
Removal
WARNING:
Electric vehicles damaged by a crash may have compromised
high voltage safety systems and present a potential high voltage
electrical shock hazard...
Other information:
Transmission Assembly
Item
Part Number
Description
1
79027902
Torque converter
2
W714629W714629
Transmission fluid pan stud bolts (6 required)
3
W500215W500215
Transmission fluid pan bolts (12 required)
4
7A1947A194
Transmission fluid pan
5
7A1917A191
Transmission fluid pan gasket
6
7E3897E389
Transmission fluid level indicator and plug assembly
7
W708500W708500
Transmission fluid auxiliary pump tube bolt (model dependent)
8
7A2097A209
Transmission fluid auxiliary pump tube (model dependent)
9
W718548W718548
Transmission fluid auxiliary pump bolts (3 required) (model dependent)
10
7P0867P086
Transmission fluid auxiliary pump (model dependent)
11
7J1357J135
Transmission fluid auxiliary pump tube seal (model dependent)
12
W700123W700123
Transmission fluid filter bolt (71 mm length)
13
W500214W500214
Transmission fluid filter bolt (20 mm length)
14
7G1867G186
Transmission fluid filter
15
W708500W708500
Main control-to-transmission case bolts (68 mm length) (8 required)
16
7A1007A100
Main control assembly
17
7N2657N265
Main control-to-transmission fluid pump seal
18
7M1837M183
Intermediate Speed A (ISSA) sensor
19
7M1017M101
Turbine Shaft Speed (TSS) sensor
20
7H1037H103
Intermediate Speed B (ISSB) sensor
21
7H1037H103
Output Shaft Speed (OSS) sensor
22
W500213W500213
Transmission internal wiring harness bolts (2 required)
23
7G2767G276
Transmission internal wiring harness
24
W500215W500215
Transmission fluid pump bolts (4 required)
25
7A1037A103
Transmission fluid pump
26
7Z3027Z302
Transmission fluid pump seal
27
66586658
Transmission fluid pump driven gear outer cover
28
W718158W718158
Transmission fluid pump retaining ring
29
7A0807A080
Transmission fluid pump driven gear
30
W504755W504755
Transmission fluid pump driven gear inner cover bolts (2 required)
31
66586658
Transmission fluid pump driven gear inner cover
32
7K4407K440
Output shaft flange nut (RWD only)
33
7A0217A021
Output shaft flange (RWD only)
34
7N1357N135
Anti-ting washer (RWD only)
35
7G1007G100
Manual control shaft-to-Transmission Range (TR) sensor roll pin
36
W712713W712713-S442-S442
Park override lever nut
37
7J1677J167
Park override lever
38
7C4937C493
Manual control shaft
39
7H5577H557
Transmission Range (TR) sensor
40
7L2527L252
Park return spring
41
7D4107D410
Park pawl actuator rod
42
W716607W716607
Transmission Range (TR) sensor detent spring bolt
43
7E3327E332
Transmission Range (TR) sensor detent spring
44
7N1347N134
Front support assembly bolts (12 required)
45
7G0337G033
Front support assembly
46
7M1577M157-C-C
B clutch (overdrive) snap ring
47
7C5767C576
B clutch (overdrive) pressure plate
48
7B4427B442-A-A
B clutch (overdrive) steel plates (quantity model dependent)
49
7B1647B164
B clutch (overdrive) friction plates (quantity model dependent)
50
7J4027J402
B clutch (overdrive) separating springs (quantity model dependent)
51
7B4427B442-B-B
B clutch (overdrive) apply plate
52
7G2067G206
One-Way Clutch (OWC)
53
7G4187G418
B clutch (overdrive) piston
54
7N1697N169
A clutch (intermediate) piston return spring snap ring
55
7G2977G297
A clutch (intermediate) piston return spring
56
7J0157J015
A clutch (intermediate) piston
57
7F2257F225
A clutch (intermediate) piston inner seal
58
7F2247F224
A clutch (intermediate) piston outer seal
59
7B0317B031
Front support-to-case seal
60
7M1577M157-J-J
Torque converter hub seal snap ring
61
7A2487A248
Torque converter hub seal
62
W500204W500204
Front support cover and seal assembly bolt
63
7M1577M157
Front support cover and seal assembly snap ring
64
75707570
Front support cover and seal assembly
65
7F0737F073
Transmission fluid pump drive gear
66
66516651
Transmission fluid pump idler gear
67
7Z4267Z426
Transmission fluid pump idler gear bearing
68
7G0907G090
Stator support seal
69
—
Clutch and planetary assembly
70
7P0807P080
A clutch (intermediate) wave spring
71
7A4067A406
A clutch (intermediate) apply plate (select fit)
72
7F2197F219
A clutch (intermediate) friction plates (quantity model dependent)
73
7F2207F220
A clutch (intermediate) steel plates (quantity model dependent)
74
7G1597G159
A clutch (intermediate) separating springs (quantity model dependent)
75
7B4377B437
A clutch (intermediate) pressure plate
76
7J3007J300
Selective shim
77
7H0327H032
Thrust bearing (T3)
78
7M1527M152-A-A
Thrust bearing (T9)
79
7A0497A049
Output shaft and planetary carrier No...
WARNING: Vehicle modifications
involving braking system, aftermarket roof
racks, suspension, steering system, tire
construction and wheel and tire size may
change the handling characteristics of your
vehicle and may adversely affect the
performance of the electronic stability
control system...

 Removal and Installation - Inner Quarter Panel