Lincoln Aviator: Body Repairs - General Information / General Procedures - Corrosion Prevention
Special Tool(s) / General Equipment
| Rust Protection Coating Gun | |
| Undercoating Gun |
Materials
| Name | Specification |
|---|---|
| ValuGard™ Premium Undercoating VG101, VG101A |
- |
| ValuGard™ Rust Inhibitor VG104, VG104A |
- |
| Motorcraft® Metal Surface Prep Wipes ZC-31-B |
- |
Repair
NOTE: Undercoating
NOTE: The following illustrations are not vehicle specific and are intended for reference only.
-
Refer to: Body Repair Health and Safety and General Precautions (100-00 General Information, Description and Operation). WARNING:
Before beginning any service procedure in this
section, REFER to Safety Warnings in section 100-00 General Information.
Failure to follow this instruction may result in serious personal
injury.
-
Wire brush the area and make sure the surfaces are free
of oil, dirt and other foreign material. Carry out the undercoating
process in the following sequence.
-
Thoroughly clean and degrease metal surfaces to remove wax and grease.
Material: Motorcraft® Metal Surface Prep Wipes / ZC-31-B
-
For best results, the vehicle should be at room temperature.
-
Attach the undercoating canister to the dispensing gun.
Use the General Equipment: Undercoating Gun
Material: ValuGard™ Premium Undercoating / VG101, VG101A
-
Undercoating should be applied after the welding and refinishing process. Product cannot be welded through.
-
Air pressure setting for applicator gun is 552 kPa (80.06 psi) – 621 kPa (90.07 psi).
-
Apply light mist coats, applicator sprays in fogging pattern. Material displaces moisture.
-
Clean up any overspray with a mild solvent such as mineral spirits or bug and tar remover.
-
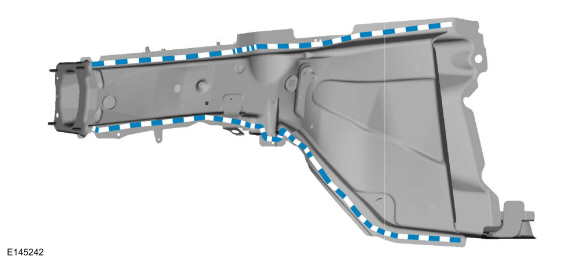
NOTE: Frame rail exterior spot-weld flange view.
Apply Premium Undercoating material to the exterior exposed edges after carrying out the welding and refinishing process.
 |
-
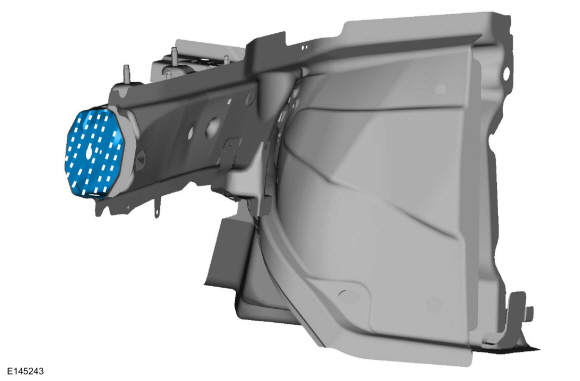
NOTE: Cross section view of typical unibody frame rail shown.
Apply Rust Inhibitor to the inner surfaces of the rail after carrying out welding process. Depress trigger and wait 2-3 seconds and slowly pull the wand to make sure the area is completely fogged.
 |
-
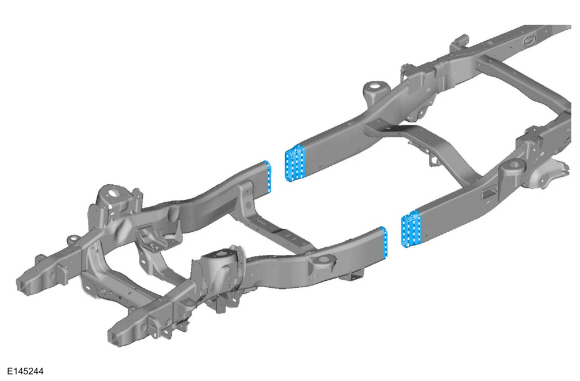
NOTE: Full frame vehicle, front rail-to-mid rail section repair shown.
Apply Premium Undercoating to the exposed surfaces after carrying out the welding process. Make sure to completely cover any bare metal areas.
 |
Repair
NOTE: Rust Inhibitor
-
The surfaces must be free of oil, dirt and other foreign
material. Carry out the process in the following sequence.
-
Thoroughly clean and degrease metal surfaces to remove wax and grease.
Material: Motorcraft® Metal Surface Prep Wipes / ZC-31-B
-
For best results, the vehicle should be at room
temperature. Attach the rust inhibitor canister to the dispensing gun.
Use the General Equipment: Rust Protection Coating Gun
Material: ValuGard™ Rust Inhibitor / VG104, VG104A
-
Rust inhibitor should be applied after the welding and refinishing process. Product cannot be welded through.
-
Air pressure setting for applicator gun is 448 kPa (64.97 psi) - 517 kPa (74.98 psi).
-
Use the appropriate length wand when spraying enclosed
areas. Insert the wand as far as possible into the access hole, pull the
trigger and wait 2-3 seconds and slowly pull the wand out of the access
hole. Apply the material in light mist coats. Material displaces
moisture.
-
Clean up any overspray with a mild solvent such as mineral spirits or bug and tar remover.
-
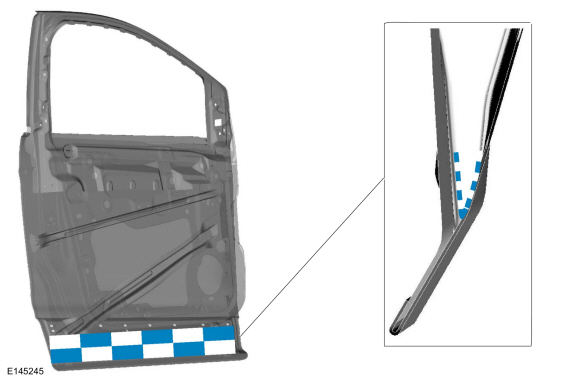
NOTE: Door assembly lower view.
Apply as shown to the inside of the door shell on all the interior metal surfaces using the most suitable applicator wand. Apply material to the exposed edges after carrying out the welding process. Make sure horizontal surfaces are well protected as they are more susceptible to corrosion. Keep door drain holes clear to prevent moisture buildup.
Material: ValuGard™ Rust Inhibitor / VG104, VG104A
 |
-
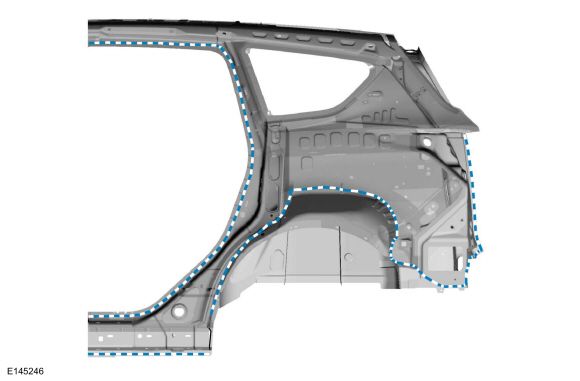
NOTE: Quarter panel inner view.
Apply to the closed channel portion of the spot weld flange areas. Apply to the exposed edges after carrying out the welding process. Make sure horizontal surfaces are well protected as they are more susceptible to corrosion.
Material: ValuGard™ Rust Inhibitor / VG104, VG104A
 |
-
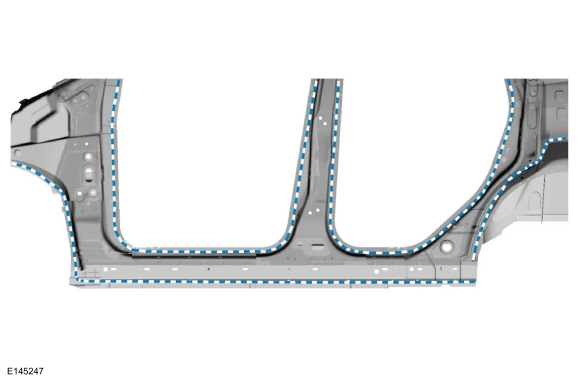
NOTE: Door frame opening view.
Apply to the closed channel portion of the spot weld flange areas. Make sure horizontal surfaces are well protected as they are more susceptible to corrosion.
Material: ValuGard™ Rust Inhibitor / VG104, VG104A
 |
 Description and Operation - Sealer, Underbody Protection Material and Adhesives
Adhesives
The
correct adhesive bonding is essential to repairing the vehicle
correctly. Adhesives and mechanical fasteners are used in certain areas
of the body structure in place of welding...
 General Procedures - Joining Techniques
Special Tool(s) /
General Equipment
Resistance Spotwelding Equipment
Spherical Cutter
Grinder
Plasma Cutter
Air Body Saw
8 mm Drill Bit
MIG/MAG Welding Equipment
Spot Weld Drill Bit
Materials
Name
Specification
Metal Bonding AdhesiveTA-1, TA-1-B, 3M™ 08115, LORD Fusor® 108B
-
Seam SealerTA-2-B, 3M™ 08308, LORD Fusor® 803DTM
-
Motorcraft® Metal Surface Prep WipesZC-31-B
-
Repair
NOTE:
Weld Bonding-Squeeze Type Resistance Spot Welding (STRW) Method...
Other information:
Lincoln Aviator 2020-2026 Service Manual: Description and Operation - About this Manual
Introduction WARNING: Before beginning any service procedure in this manual, refer to health and safety warnings in section 100-00 General Information. Failure to follow this instruction may result in serious personal injury. For additional information, refer to: Health and Safety Precautions (100-00 General Information, Description and Operation)...
Lincoln Aviator 2020-2026 Service Manual: Description and Operation - Vehicle Specific Body Construction
For recommended metal repair guidelines and recommendations, refer to the following illustrations and: For additional information, refer to: Specifications (501-25 Body Repairs - General Information, Specifications). Steel Type Legend Item Steel Type Color 1 Mild Steel Yellow 2 Bake Hardened Steel (BH) Light Blue 3 Solid Solution Strength Pink 4 High Strength Low Alloy (HSLA) Dark Blue 5 Dual Phase (DP) 500, 600 Class Steel Green 6 Dual Phase (DP) 700, 800, 900, 1000 Class Steel Fuchsia 7 Laminate Steel Teal 8 Ultra High Strength Steel (UHSS) Martensitic, Boron Red 9 Transformation Induced Plasticity Steel (TRIP) Gold 10 Aluminum Purple Front Structure Item Description Steel Type 1 Radiator support Magnesium alloy 2 Bracket High-Strength Low Alloy (HSLA) 350 steel 3 Bracket Aluminum alloy 4 Suspension housing Aluminum alloy 5 Reinforcement High-Strength Low Alloy (HSLA) 350 steel 6 Reinforcement Boron and Dual Phase (DP) 600 steel 7 Reinforcement Boron and Dual Phase (DP) 600 steel 8 Bracket Aluminum alloy 9 Side member assembly Aluminum alloy 10 Fender apron tube Dual Phase (DP) 800 steel Front Bumper Item Description Steel Type 1 Bumper assembly High strength aluminum Dash Panel and Front Fenders Item Description Steel Type 1 Crossmember Boron steel 2 Dash panel Mild steel 3 Cowl top panel Mild steel 4 Reinforcement Dual Phase (DP) 800 steel 5 Front crossmemembr extension Dual Phase (DP) 600 steel 6 Reinforcement Dual Phase (DP) 800 steel 7 Fender assembly (LH/RH) Bake Hardened (BH) 210 steel 8 Bracket Mild steel Body Side Inner Panels NOTE: Left hand (LH) side shown, right hand (RH) side similar...
Categories
- Manuals Home
- Lincoln Aviator Owners Manual
- Lincoln Aviator Service Manual
- Fuel Quality
- Interior Lamps
- Description and Operation - Body and Frame
- New on site
- Most important about car
Activating Intelligent Access
The intelligent access key must be within 3 ft (1 m) of the door or luggage compartment you intend to lock or unlock.
At a Door
Electronic door handles are on each door. Gently depress the switch inside the exterior door handle to unlock and open the door. An unlock symbol illuminates on the door window trim indicating your vehicle is unlocked.